10 Steps to Specify an ERW Tube Mill: Tube Size to Full Line
Choose the mill model from your maximum OD and wall thickness, then use strip, material, coil, speed, cutting, power and site data to define the full line.
Read article04 · STRIP JOINING
At a coil change, the shear and butt welder trims and joins the strip ends. When its cycle fits usable accumulator storage, downstream production continues.
 Illustrative render Its place in the line
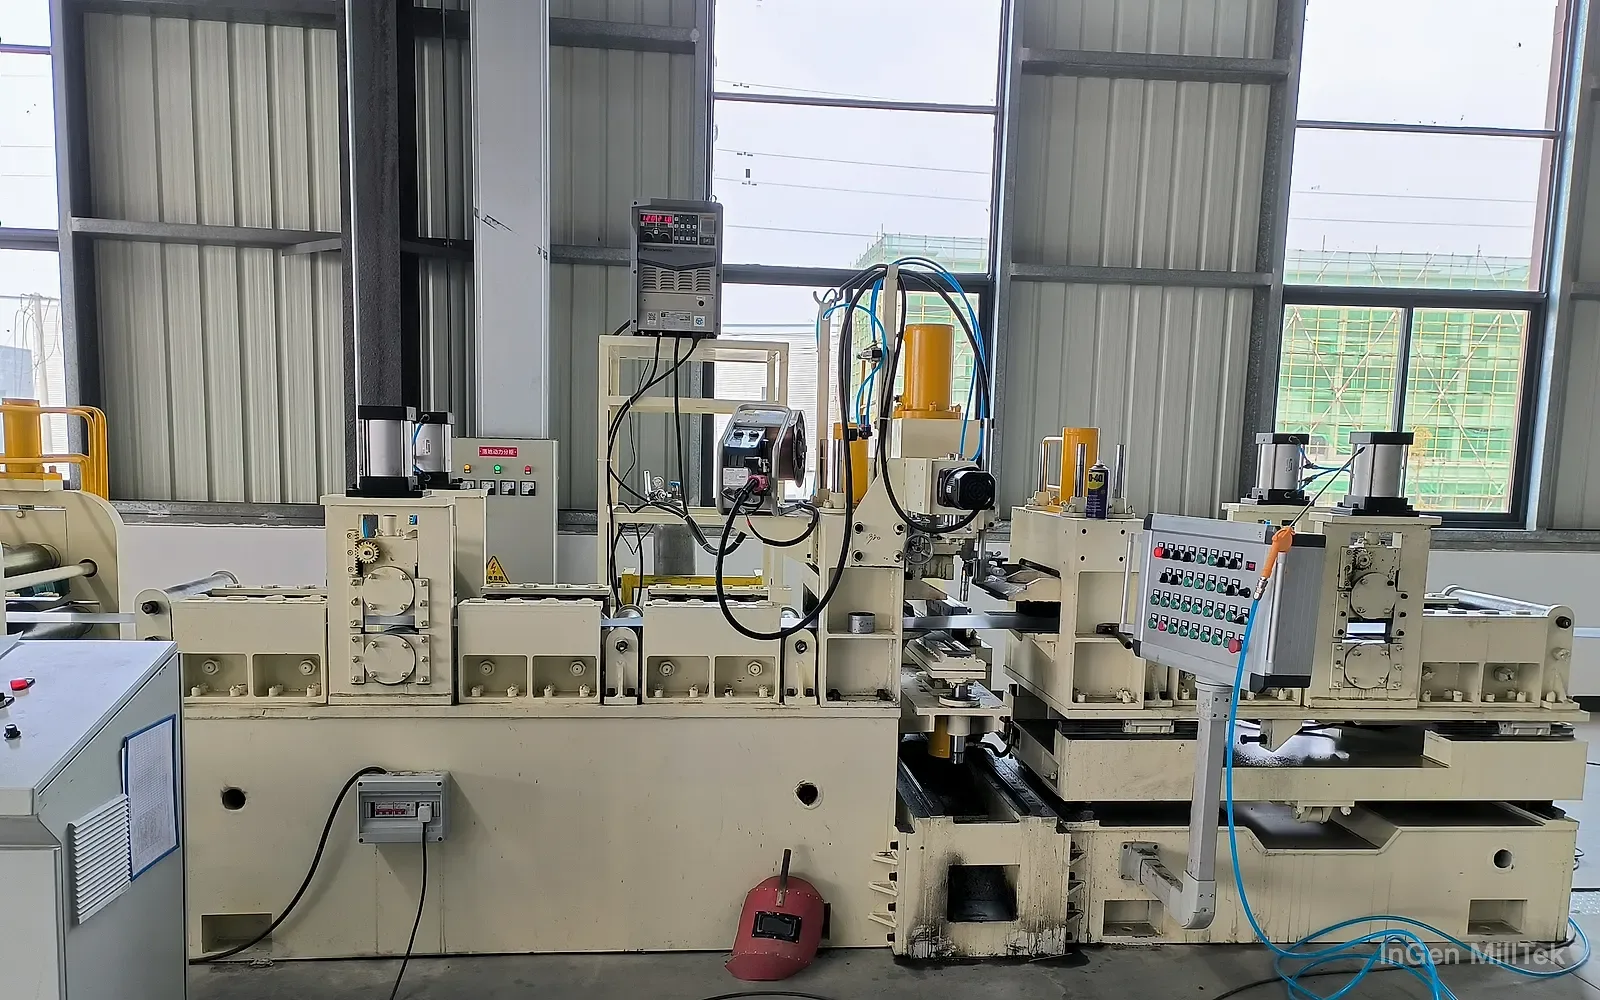
When a coil runs out, the shear and butt welder trims, aligns and joins the old coil tail and the new coil head into continuous strip, reducing the need for re-threading. The downstream mill can continue during the entry interruption when the joining cycle matches the usable accumulator storage. It is a key machine for coil-change efficiency on a continuous line.
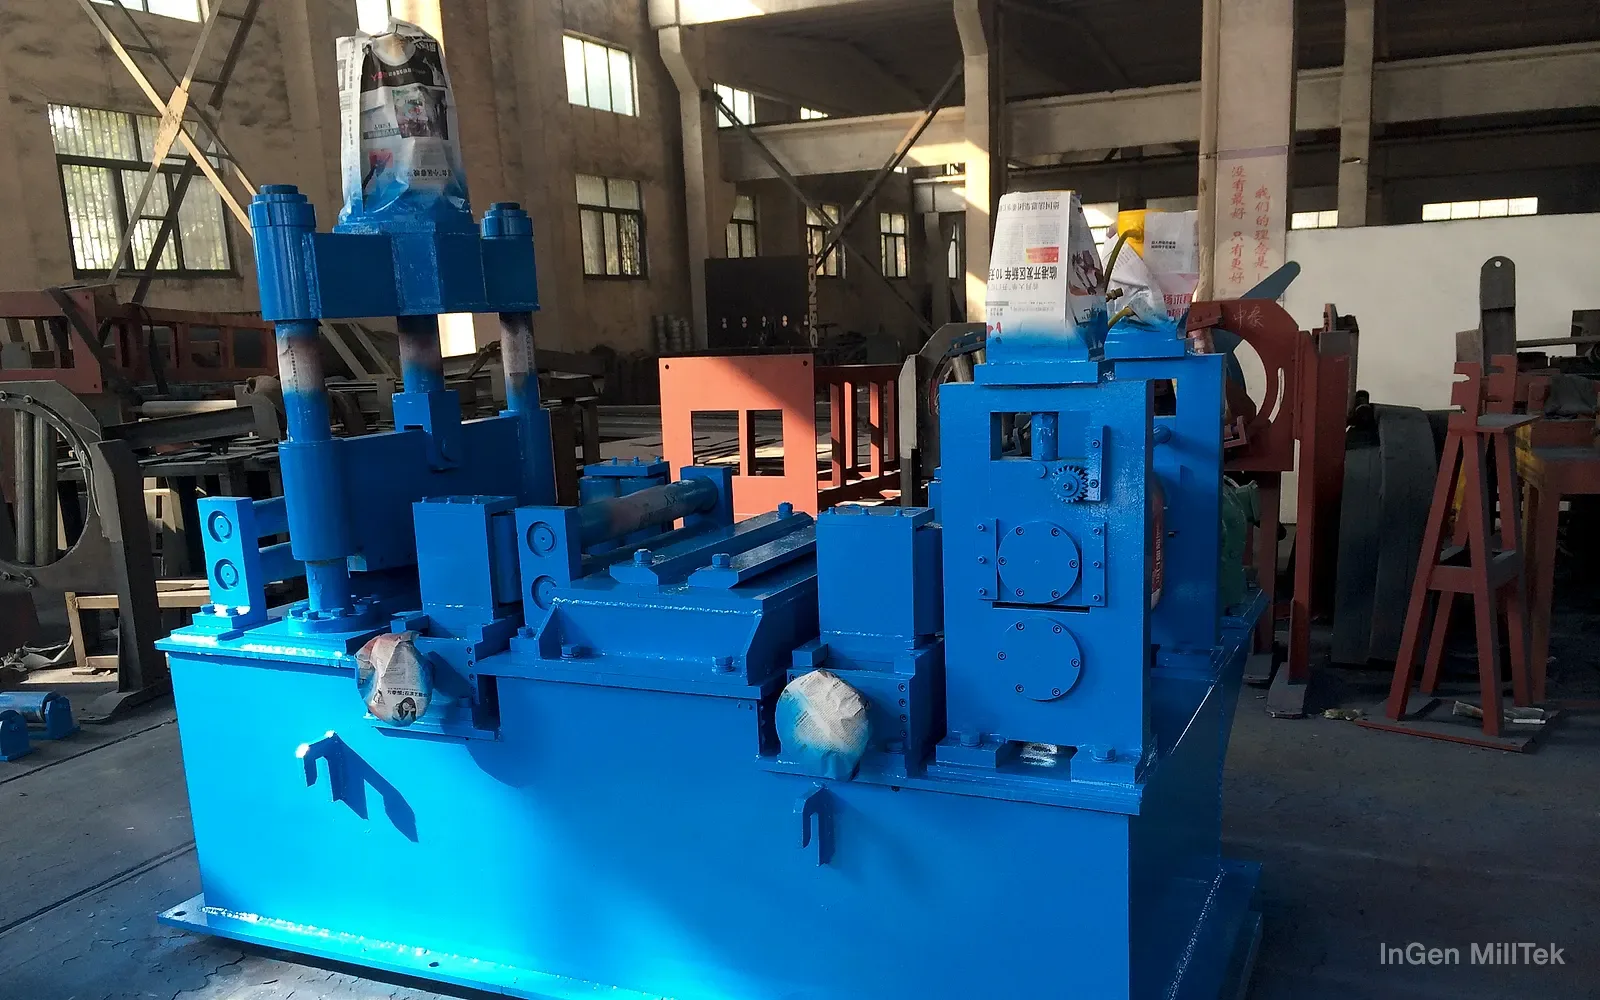
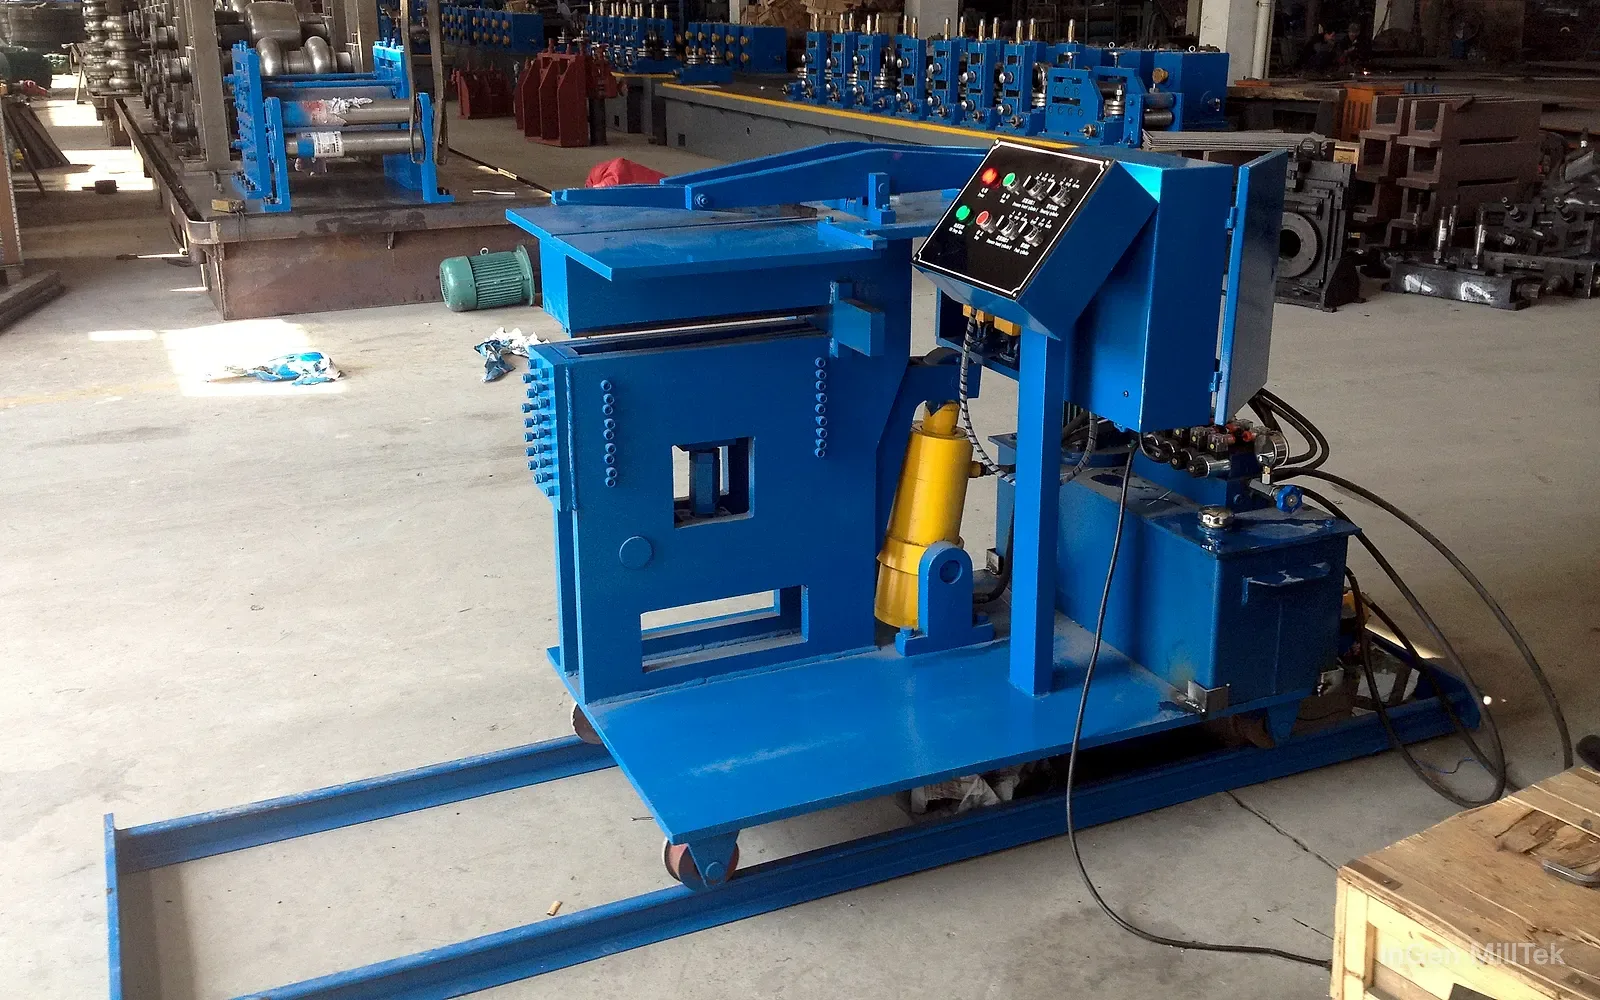
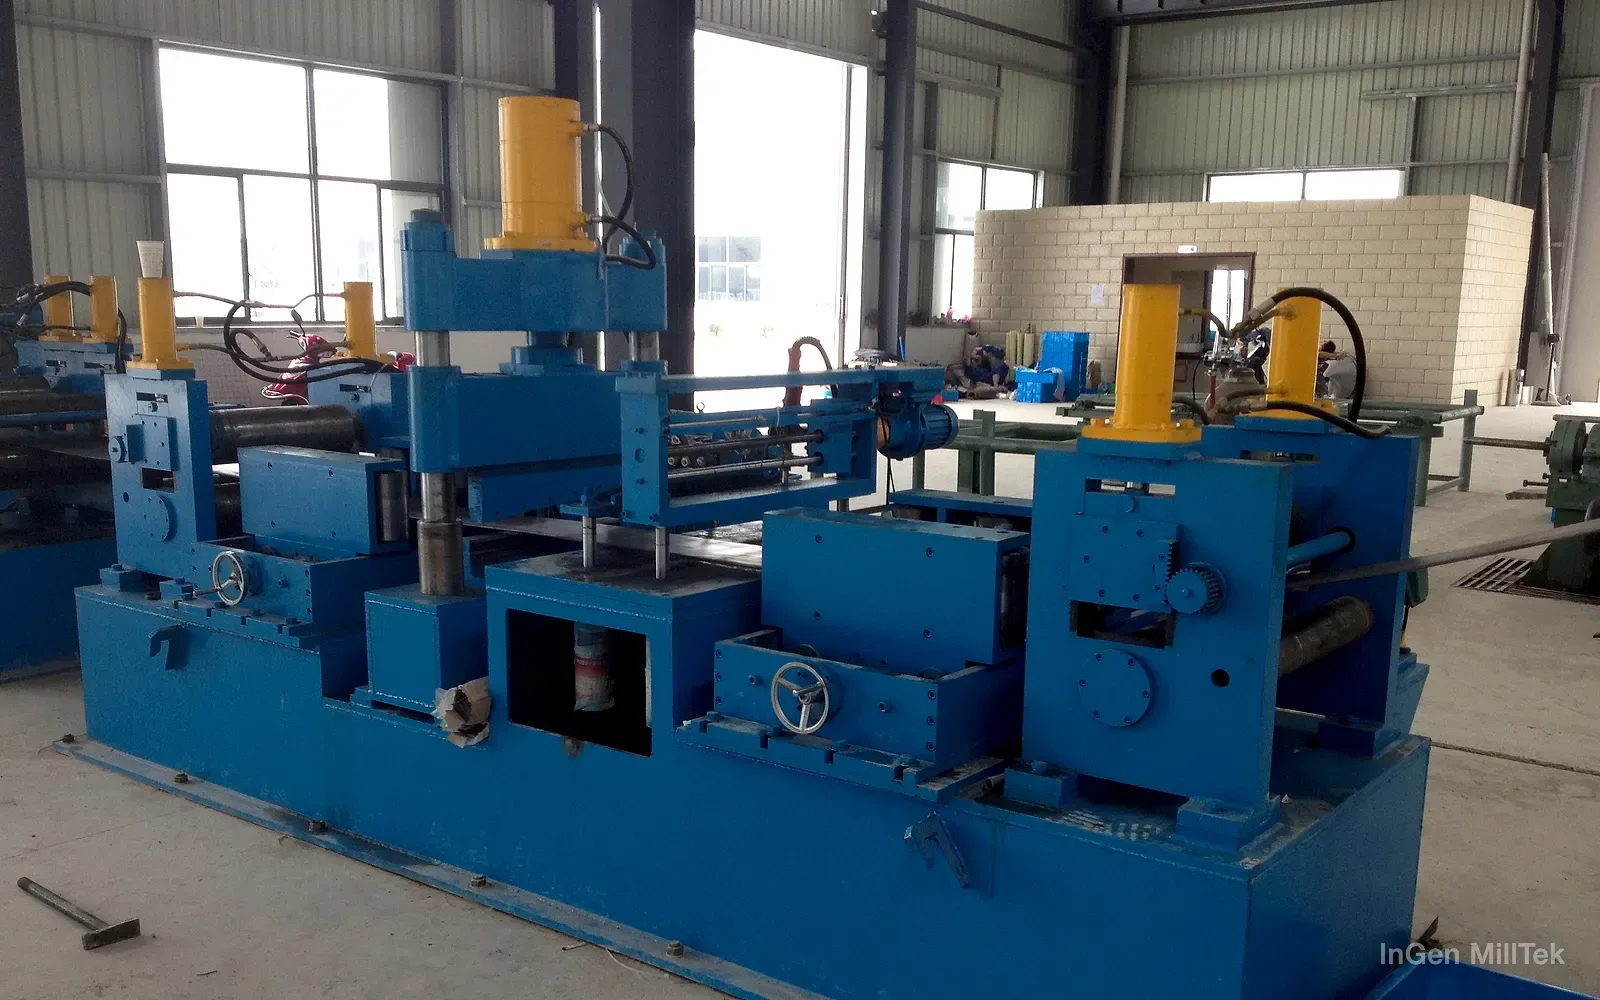
We build shear and butt welders in three grades, set by how the strip is welded and how much is automated. The Integrated Shear & Manual Welder has a hydraulic shear, manual alignment (assisted alignment on the gantry version) and manual welding; the hydraulic-shear version uses the customer's own welder, and twin-column and gantry versions are built for wide or thick strip. The Semi-automatic Shear & Welder has a hydraulic shear, manual alignment and a wire-feed welder for electrically controlled welding. The Fully Automatic Shear & Welder shears, aligns and welds automatically, reducing the corresponding manual operations.
Selection depends on strip width, thickness and material, and on the joint quality required: the weld has to survive the forming rollers downstream without cracking. Lines with frequent coil changes or few operators benefit from the semi-automatic or fully automatic grade. The width and thickness range of each grade is in the table below.
Joining time includes more than welding: strip-end positioning, trimming, alignment, clamping, welding and release all contribute to the cycle. Assess accumulator buffering against the actual operating cycle rather than treating one action time as the entire coil-change duration.
Confirm the joint material, dimensions and downstream path together, including passage through the accumulator and forming rollers and any required joint identification or handling. Record the strip, joining method, joint inspection and downstream passage during acceptance; completing one weld does not establish the whole acceptance result.
Used in these lines Tube mill lines · 12 models, complete lines
Contact us to confirm specifications for your production requirements.
| Grade and construction | Strip width mm | Strip thickness mm |
|---|---|---|
| Integrated Shear & Manual WelderHydraulic shear, customer's own welder | ≤220 | ≤3 |
| ≤260 | ≤4 | |
| ≤320 | ≤4 | |
| ≤450 | ≤4 | |
| ≤520 | ≤4 | |
| ≤620 | ≤4 | |
| Integrated Shear & Manual WelderTwin-column shear, wide or thick strip | ≤400 | ≤6 |
| ≤500 | ≤6 | |
| ≤600 | ≤8 | |
| ≤700 | ≤8 | |
| ≤800 | ≤12 | |
| ≤900 | ≤14 | |
| Integrated Shear & Manual WelderGantry, assisted alignment, wide or thick strip | ≤500 | ≤6 |
| ≤600 | ≤8 | |
| ≤700 | ≤10 | |
| ≤800 | ≤12 | |
| ≤900 | ≤14 | |
| Semi-automatic Shear & WelderHydraulic shear with wire-feed welder | ≤160 | ≤3 |
| ≤220 | ≤4 | |
| ≤320 | ≤4 | |
| ≤420 | ≤4 | |
| ≤520 | ≤4 | |
| Fully Automatic Shear & WelderAutomatic shearing, alignment and welding | ≤350 | ≤4 |
| ≤500 | ≤6 | |
| ≤600 | ≤6 | |
| ≤700 | ≤8 | |
| ≤800 | ≤10 | |
| ≤1000 | ≤10 |
The grades differ in how the strip is welded and how much is automated. Integrated Shear & Manual Welder: hydraulic shear, manual (or assisted) alignment and manual welding. Semi-automatic Shear & Welder: hydraulic shear and manual alignment with an automatic wire-feed welder (electrically controlled welding). Fully Automatic Shear & Welder: automatic shearing, alignment and welding. Widths and thicknesses are the upper limits of each size.
A gantry semi-automatic version (hydraulic shear + assisted alignment + wire-feed welding) is configured per project for wide or thick strip.
Source: company product catalogue (April 2025 edition), page 8.
Use these points to prepare the equipment discussion. Specifications and configuration depend on the project.
We discuss the suitable model and configuration for your product and plant. Every line is configured per project, and pricing follows the configuration.